Laser Control Pyrometer
The HELISYS Laser Control System
Ultra-fast infrared temperature measurement devices optimized for use in additive manufacturing processes. They optimize all laser-based applications by either monitoring processes or controlling them to a setpoint in near real-time based on the measured temperature. The H4 measures, thinks and acts directly in the housing and passes the finished correction signal (an analog 0–10 V signal) directly to the laser.
Can be integrated into existing laser heads
Measures the melt pool temperature directly at the laser impact point
Controls laser power at points where the laser would otherwise burn the material during changes in direction
What can you do with it?
High-SpeedLlaser Cladding – Ultra-Fast & Flawless Coatings
Ultra-fast coating, perfectly controlled: The H4 controls melt pool temperatures in microseconds even at extreme feed rates – ensuring flawless, ultra-thin protective layers.
Prevents thermal overheating of the underlying substrate material.
Matches energy input precisely to the dynamic high-speed powder flow.
Ensures uniform layer thickness and a flawless metallurgical bond.
High-speed laser cladding with an off-axis coupled pyrometer optics
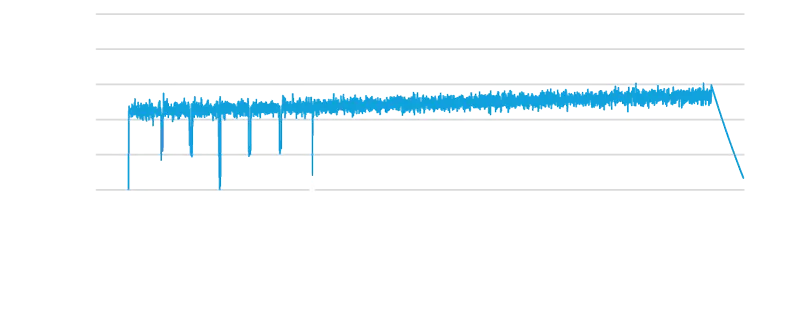
High-speed laser cladding with an koaxial coupled pyrometer optics
LMD – High-Precision Metal Deposition
Consistent quality with every track: Whether for repair or 3D shaping, the integrated PID controller prevents heat accumulation as part height increases, securing a homogenous microstructure.
Minimizes residual stress and thermal distortion in the component.
Guarantees optimal fusion between the deposited metal and base material.
Maintains consistent track width and height throughout the process.
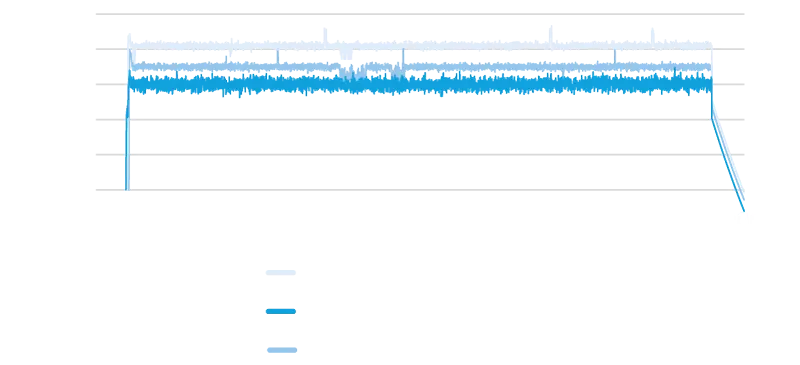
Laser metal deposition temperature coaxial coupled, PID controlled
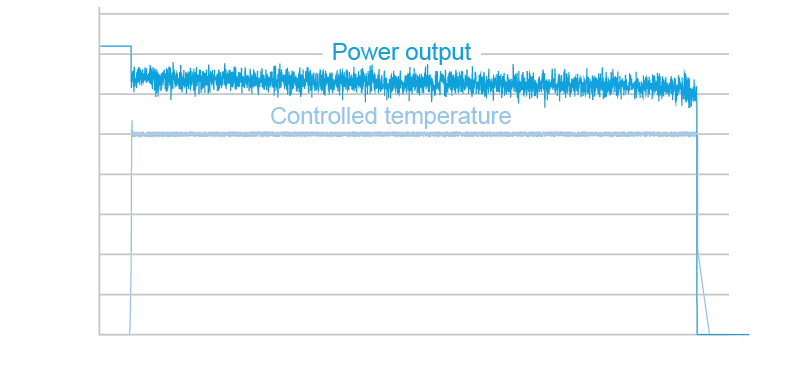
The surface temperature is extremely constant because the PID controller continuously adjusts its power output to the heating component.
LPBF – Intelligent Powder Bed Control
Real-time control in the powder bed: Eliminate scrap at overhangs and sharp corners – the H4 adjusts laser power in-track and in real time to match local thermal conditions.
Eliminizes temperature drift during long, complex build cycles.
Optimizes melt pool stability via ultra-fast, real-time power adjustment.
Prevents critical defects like micro-cracks and structural delamination.
To sum up very briefly:
Highspeedpyrometer sind verfügbar als:
- 1-color pyrometers with an exposure time < 20 µs for over 50000 measurements / s (50 kHz measurement frequency).
- H3-2-color pyrometers with an exposure time of <40 µs for over 25000 measurements / s (50 kHz measurement frequency).
- H4-2-color pyrometers with an exposure time < 25 µs for over 40,000 measurements/s (40 kHz measurement frequency).
-
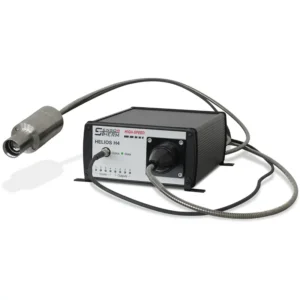
HELIOS H422 (High-Speed 2-Color Pyrometer)
Temp. range 700 – 2300°C / 1292 – 4172°F
Spectral range 1.45 – 1.8 µm; < 50 µs fast
Smallest spot size 0.8 mm
Ethernet, switching inputs/outputs -
HELIOS H433 (High-Speed 2-Color Pyrometer)
Temp. range 700 – 2300°C / 1292 – 4172°F
Spectral range 1.6 – 2.1 µm; < 50 µs fast
Smallest spot size 0.8 mm
Ethernet, switching inputs/outputs -
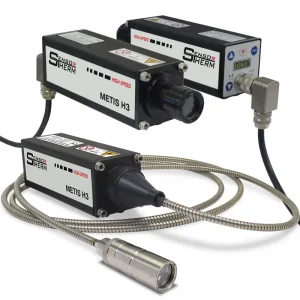
METIS H322 (High-Speed 2-Color Pyrometer)
8 temp. ranges betw. 350 and 3000°C / 662 and 5432°F
Spectral range 1.45 – 1.8 µm; < 80 µs fast;
Smallest spot size 0.8 mm
Display, adjustm. buttons, switching inputs / outputs -
METIS H311 (High-Speed 2-Color Pyrometer)
7 temp. ranges betw. 600 and 3300°C / 1112 and 5972°F
Spectral range 0.75 – 1.1 µm; < 80 µs fast;
Smallest spot size 0.8 mm
Display, adjustm. buttons, switching inputs / outputs -
METIS H318 (High-Speed 1-Color Pyrometer)
2 temp. ranges betw. 120 and 800°C / 248 and 1472°F
Spectral range 1.65 – 2.1 µm; < 40 µs fast;
Smallest spot size 0.4 mm
Display, adjustm. buttons, switching inputs / outputs -
METIS H316 (High-Speed 1-Color Pyrometer)
7 temp. ranges betw. 250 and 2500°C / 482 and 4532°F;
Spectral range 1.45 – 1.8 µm; < 40 µs fast;
Smallest spot size 0.4 mm
Display, adjustm. buttons, switching inputs / outputs -
METIS H309 (High-Speed 1-Color Pyrometer)
5 temp. ranges betw. 550 and 2000°C / 1022 and 3632°F
Spectral range 0.7 – 1.1 µm; < 40 µs fast;
Smallest spot size 0.4 mm
Display, adjustm. buttons, switching inputs / outputs -
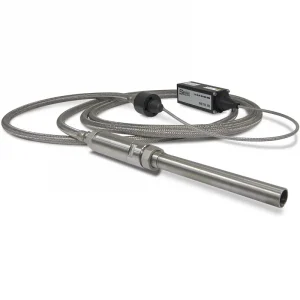
Heavy-Duty Measuring System for METIS M3 or H3 Pyrometers
Focus distance up to 4.5 m
Use up to 250°C on the measuring head
Stainless steel braided hose in lengths up to 30 m
Air purge for the optics system